Machine Automation Solutions Explained: What They Are, the Main Types, and How to Choose One
Key takeaway: Machine automation solutions are systems that let machines run production tasks — moving, cutting, assembling, checking or packing — with limited human input, using controllers such as PLCs, robots, CNC machines and sensors. The right choice depends on your product mix, volume and budget, not on buying the most advanced machine available.
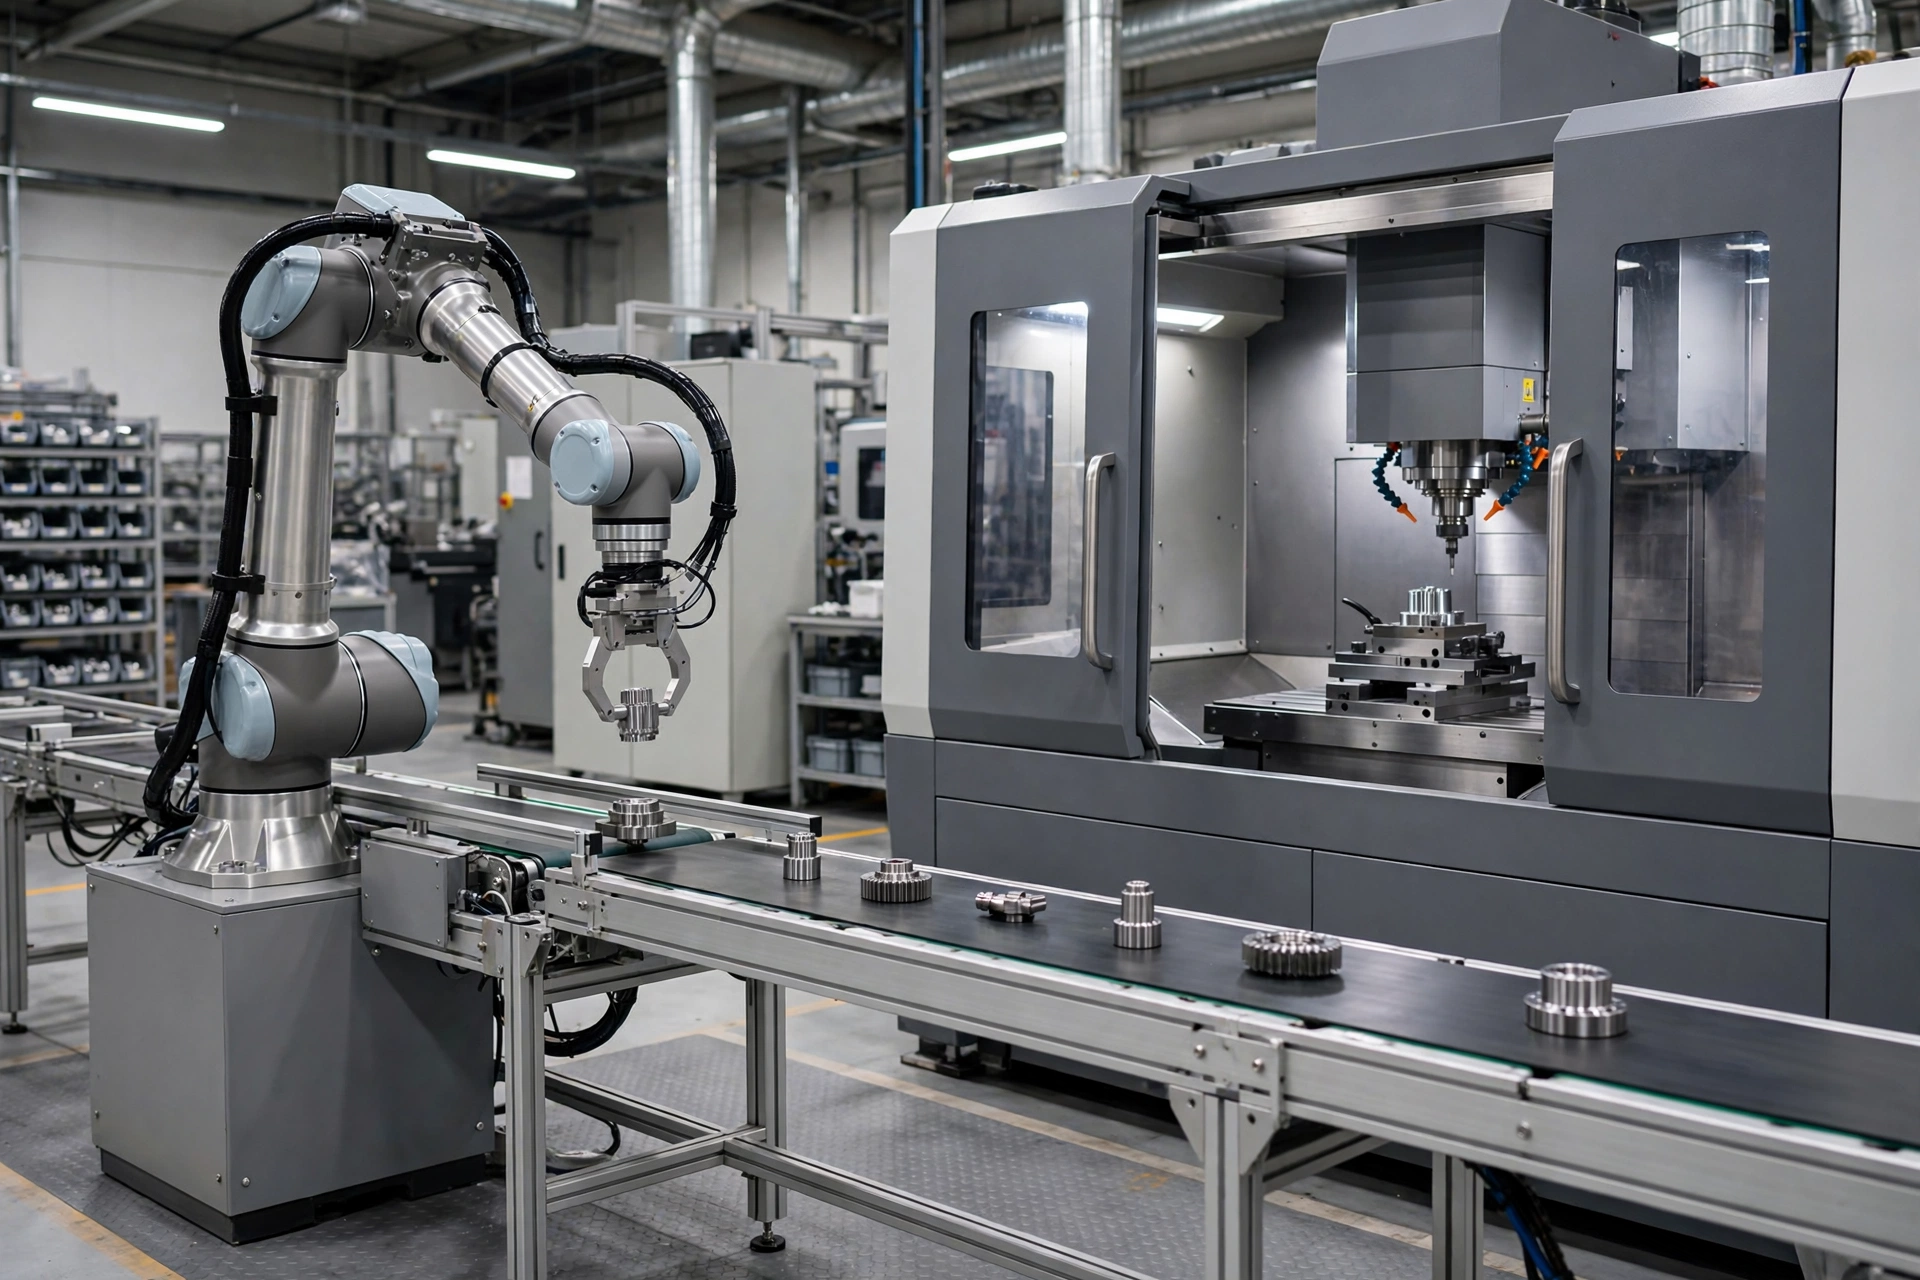
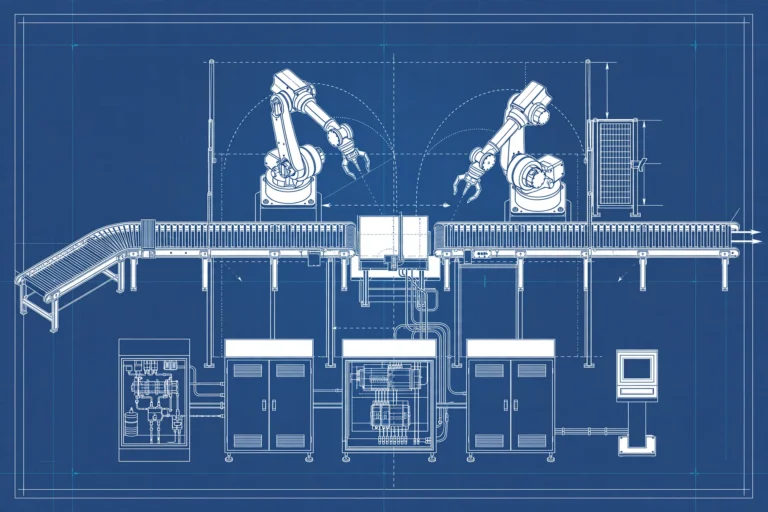
When people say “machine automation solutions”, they usually mean more than one machine. They mean a working combination: a controller that makes decisions, sensors that report what is happening, actuators that move things, and software operators can monitor. A single automated conveyor is a start. A full solution connects it to a packing machine, an inspection camera and a dashboard showing output in real time.
That distinction matters because buying hardware alone rarely fixes a production problem. If the bottleneck is inconsistent quality, a faster machine will only produce rejects faster. If the bottleneck is changeover time, a rigid high-speed line will make things worse. Start from the problem, then match the solution to it.
What machine automation solutions include
A typical solution has five parts. The controller — often a programmable logic controller (PLC) — runs the programmed logic. Sensors measure position, temperature, pressure, weight or presence. Actuators — motors, cylinders and valves — do the physical work. A human-machine interface (HMI) lets operators start, stop and adjust the process. And supervisory software, such as SCADA, collects data across machines and sites. Newer layers add industrial Internet of Things (IIoT) dashboards and machine vision, which checks products with cameras instead of eyes.
The four types of machine automation
Manufacturing automation is usually classified into four types: fixed, programmable, flexible and integrated. Fixed automation, also called hard automation, does one job repeatedly at high speed — transfer lines and dedicated assembly stations. It suits mass production but is hard and costly to change. Programmable automation can be reprogrammed for different products, which suits batch production: CNC machines and PLC-controlled cells are classic examples. Flexible automation switches between products with little or no lost changeover time, suiting varied, smaller batches. Integrated automation links whole lines under one coordinated system, with minimal human intervention.
The scale of the shift is measurable. The International Federation of Robotics (IFR) reported 542,000 industrial robots installed worldwide in 2024 — more than double the number installed ten years earlier, and the fourth straight year above 500,000. Asia accounted for 74% of new deployments, Europe 16% and the Americas 9%.
Machine automation solutions compared
The comparison in short: PLC-controlled machines suit single machines and straightforward lines, robots suit repetitive physical tasks, CNC suits precise cutting and shaping, and SCADA suits monitoring whole processes.
| Solution | Best for | Strength | Watch out for |
|---|---|---|---|
| PLC-based machine control | Single machines, conveyors, packaging lines | Reliable, well understood, easy to expand | Needs careful programming and safety design |
| Industrial robots | Welding, assembly, palletising, machine tending | Consistent, tireless, good in hazardous jobs | Guarding, integration and programming time |
| CNC machines | Cutting, drilling, milling, turning | Repeatable precision | Skilled programming and tooling costs |
| Machine vision | Defect detection, counting, barcode reading | Fast, consistent inspection | Lighting and product variation can fool cameras |
| SCADA + IIoT dashboards | Monitoring lines, plants or fleets | Visibility, alarms, trend data | Only as good as the sensors feeding it |
What machine automation solutions cost
There is no single price for machine automation, and any article quoting one without context should be treated with suspicion. A PLC retrofit on one existing machine is a small project. A robot cell with guarding, grippers and integration is a medium project. A fully integrated line with vision, conveyors and supervisory software is a large capital project, and integration — programming, safety validation and commissioning — is often a major share of the total, not an afterthought. Budget too for safety assessments, spare parts, training, software licences and downtime during installation, and compare whole-job quotes, not hardware prices alone.
What you need before you automate
Four prerequisites matter. First, a stable, documented process: current steps, cycle time and defect rate, so you can prove the automation improved them. Second, a safety plan: risk assessment, guarding, emergency stops and lockout procedures, designed in from the start. Third, people: someone who can operate the system and someone who can maintain it, or a support contract covering both. Fourth, data: decide what you will measure — output, uptime, scrap rate — and how you will read it. Automating an undocumented process usually just automates its problems.
Risks and limits of machine automation
Fixed systems lose money when product designs change. Robots need space, guarding and careful programming, and cannot improvise like a skilled operator. Vision systems struggle with reflective surfaces and variable lighting. Connected systems add cybersecurity risk: a dashboard that can see a machine should never be a door into controlling it without proper network segmentation and access controls. Automation also changes jobs rather than simply removing them — operators become supervisors, programmers and maintainers — so training must be part of the purchase, not an optional extra.
How to choose the right solution
Define the single problem you are solving and the number that proves it is solved. Walk the line and find the true bottleneck — automating a fast step while a slow step stays manual gains nothing. Pilot on one machine or cell, measure against your baseline, and only then scale. Choose a supplier on integration and support, not just hardware price: the supplier who commissions the system properly and answers the phone afterwards is worth more than the cheapest quote.
Analysis: Automation is now a menu, not a single purchase. Small manufacturers do not need a fully integrated line to benefit — a PLC retrofit or a single robot cell can be the right first step — but they do need the unglamorous prerequisites of safety, skills and measurement in place before any of it pays off.
Related reading on USABite: IoT-enabled industrial automation, technology implementation, and labour planning and automation advantages.
Sources
- International Federation of Robotics, World Robotics 2025 — 542,000 industrial robots installed in 2024, as reported by DC Velocity and Robotics and Automation Magazine.
- Four types of automation — fixed, programmable, flexible and integrated — explained by IndMall Automation and Sims Engineering.
- Industrial automation components and technologies — PLC, SCADA, HMI, robotics and sensors — covered in Astech Projects’ industrial automation guide.
Frequently asked questions
What is a machine automation solution?
A machine automation solution is a combination of controllers, sensors, actuators and software that lets machines carry out production tasks with limited human input. It can be as small as a PLC controlling one machine or as large as an integrated line with robots, vision inspection and supervisory dashboards.
What are the four types of automation?
The four types are fixed, programmable, flexible and integrated automation. Fixed automation does one job repeatedly at high speed. Programmable automation can be reprogrammed for different products. Flexible automation switches between products with little changeover loss. Integrated automation links whole processes under one coordinated system.
How much do machine automation solutions cost?
Costs vary too widely for a single figure to be meaningful. A PLC retrofit on one machine is a small project, a robot cell with guarding and integration is a medium project, and a fully integrated line is a large capital project. Always compare whole-job quotes including integration, safety, training and support, not hardware prices alone.
What is the difference between PLC automation and robotics?
PLC automation is the control logic that runs machines, conveyors and processes. Robots are the physical machines that do tasks such as welding, assembly and palletising, and they are usually controlled by a PLC or a robot controller. Most robot cells therefore include both: the robot does the work and the PLC coordinates it with the rest of the line.
Is machine automation worth it for a small manufacturer?
It can be, if it targets a clear bottleneck. A single PLC retrofit, a small robot cell or a vision inspection station can pay back where a full line would not. The key is to pilot one cell, measure output, scrap and uptime against a baseline, and scale only when the numbers prove the gain.
One Comment
Comments are closed.